Info Center
Language
The Benefits of Dried Shiitake Mushrooms
Drying shiitake mushrooms using an industrial heat pump dryer transforms a perishable fresh crop into a stable, high-value ingredient with significantly enhanced properties. The primary benefit is the dramatic extension of shelf life; properly dehydrated shiitake can be stored for over a year without refrigeration, reducing food waste and allowing growers to sell product during off-season market windows.
Beyond preservation, the drying process intensifies the mushroom's natural umami flavor profile. As moisture evaporates, the concentration of guanylate—the compound responsible for shiitake's signature savory depth—increases substantially. This makes dried shiitake a powerful flavor base for stocks, broths, and sauces.
Nutritionally, drying preserves the mushroom's essential vitamins, fiber, and minerals. In fact, when dried shiitake are exposed to UV light during the process, their Vitamin D content skyrockets, often making them a superior source compared to fresh specimens. Finally, drying reduces weight and volume by up to 90%, dramatically lowering shipping costs and carbon footprint. For commercial food processors and wholesalers, investing in dried shiitake production ensures consistent quality, year-round availability, and maximized profit margins.
Maximizing Shiitake Mushroom Preservation with
AIM Industrial Heat Pump Dryers: 100kg Capacity, Smart Control & Year-Round Savings
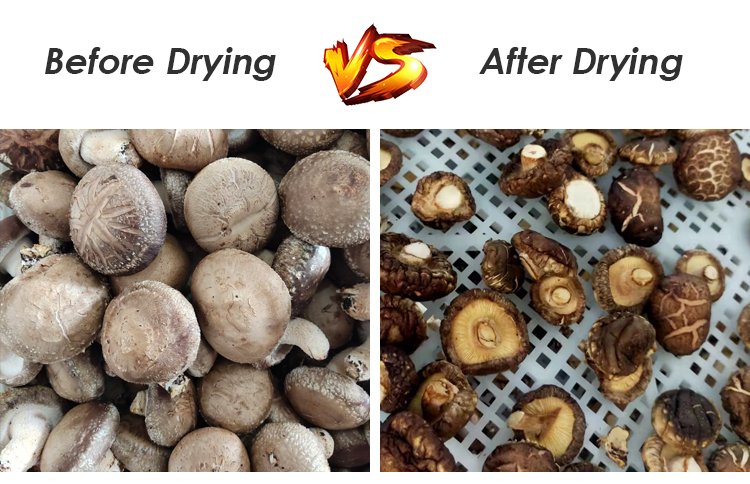
Before and After: The AIM Drying Advantage
Prior to adopting AIM drying solutions, many growers rely on traditional sun-drying or basic electric heating. Before using the AIM dryer, results are inconsistent—batches suffer from uneven moisture content, surface cracking, or discoloration caused by high-heat damage. Furthermore, relying on weather conditions risks mold development and significant crop loss.
After switching to the AIM heat pump dehydrator, the contrast is stark. The system maintains a precise, gentle airflow between 50°C and 65°C, perfectly suited for Shiitake mushroom drying. The result is a uniformly dried cap with a tight, white "cracked" pattern highly sought after by wholesale buyers. More importantly, the process locks in the mushroom's natural Guanylate compounds, intensifying the savory flavor that commands premium pricing.
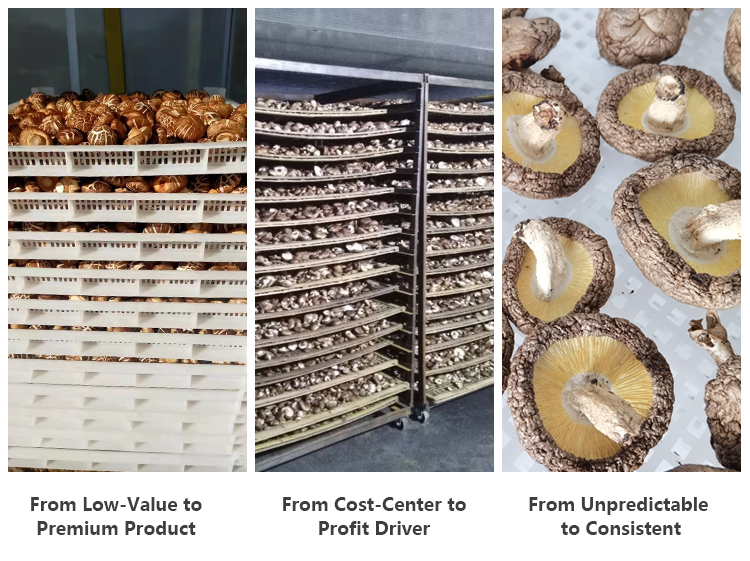
High-Capacity Efficiency Meets Low Energy Consumption
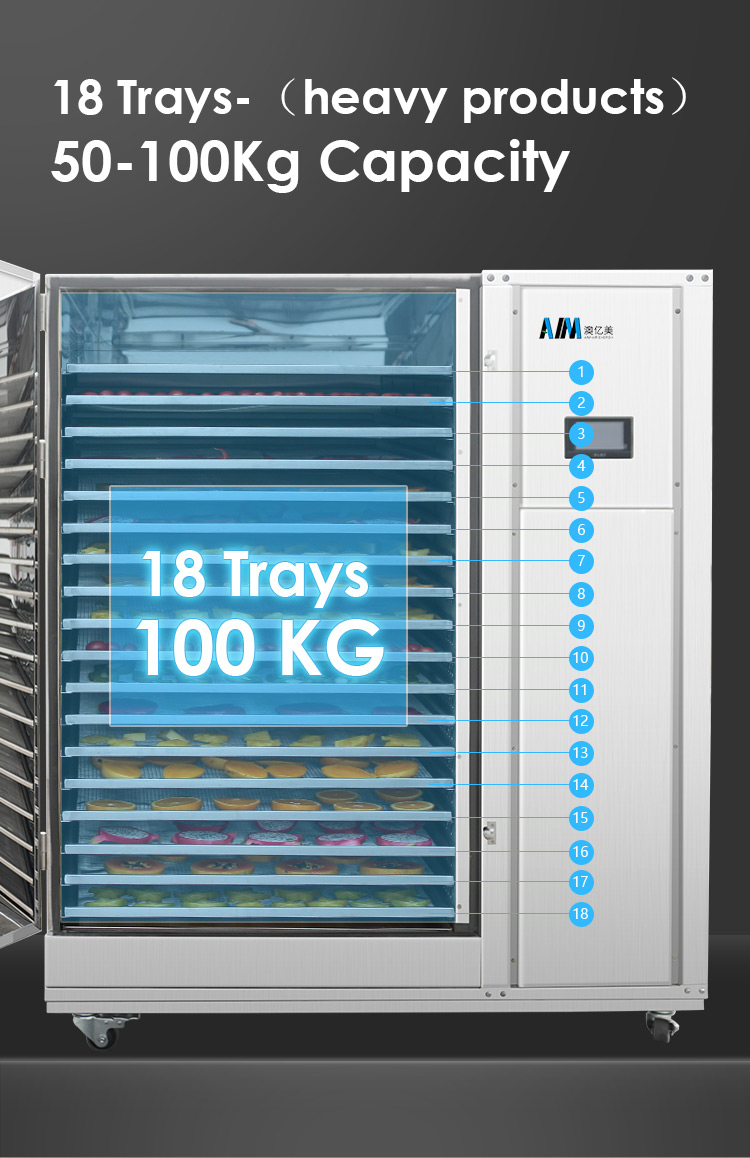
Designed for heavy-duty use, the AIM system easily handles 100kg capacity per batch, ensuring that large harvests are processed in a single, efficient cycle. For expanding enterprises, we offer larger capacity heat pump drying machines capable of handling multi-ton daily throughput. Despite this industrial scale, the energy consumption is remarkably low. Unlike gas or electric resistance heaters, our industrial food dryer utilizes a closed-loop heat pump system that recycles hot air, slashing operational costs by up to 60% compared to conventional methods.
Smart Farming: Mobile Control and Real-Time Monitoring
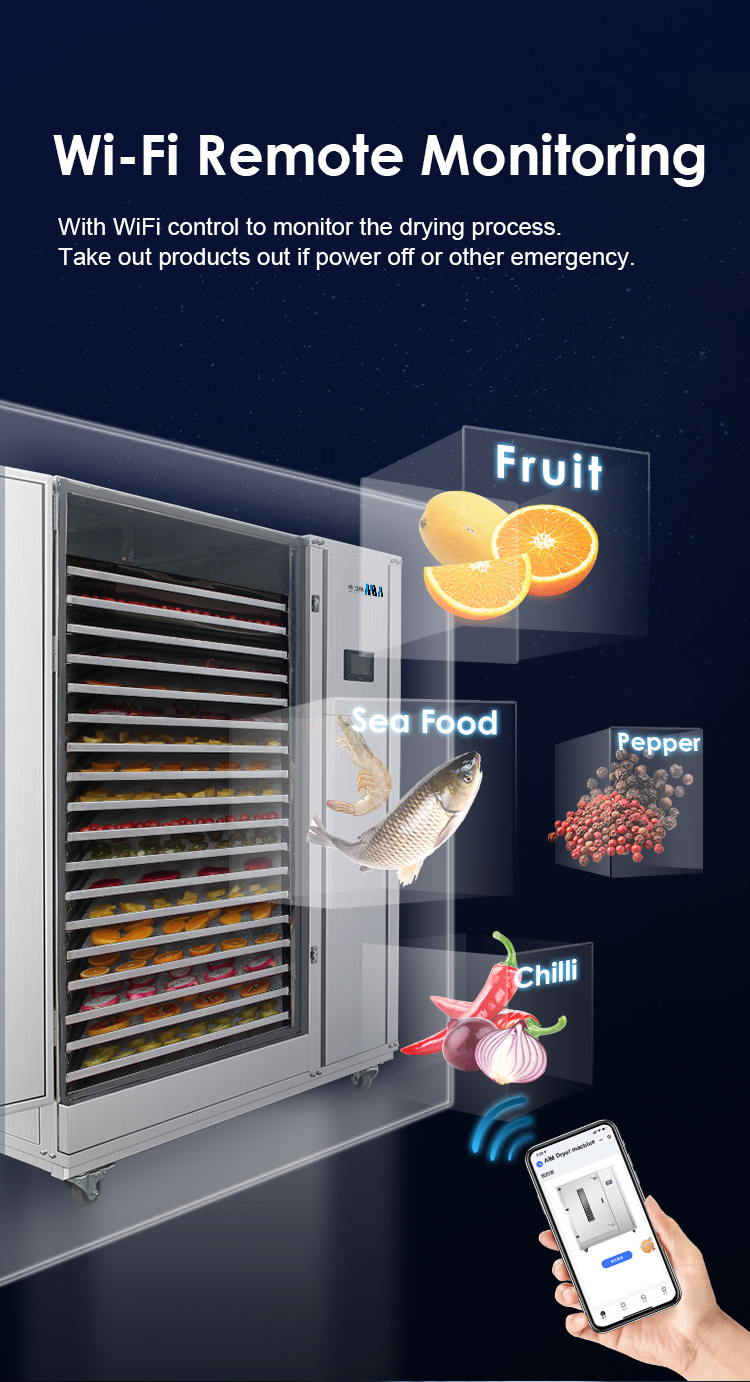
Modern agriculture requires precision beyond manual gauges. The AIM dryer is equipped with an intelligent IoT interface, allowing operators to adjust temperature and humidity curves directly from a smartphone. This real-time monitoring feature ensures that even if you are off-site, you have complete visibility over the mushroom drying process. You can adjust settings to prevent over-drying or stop the cycle the moment optimal moisture content is achieved, eliminating human error.
The Essential Tool for Agriculture, Industry, and Commerce
Whether you are a commercial farm looking to diversify revenue streams, an industrial processor producing mushroom powder, or a food exporter needing stable, lightweight cargo, the AIM heat pump food dryer is an indispensable asset. It bridges the gap between raw agricultural yield and high-value commercial product.
Ready to eliminate waste and maximize the shelf life of your shiitake harvest? Explore the efficiency of AIM 100kg heat pump dehydrators and discover the future of industrial food drying today

 sales@aimheatpump.com
 +0086-18022011556